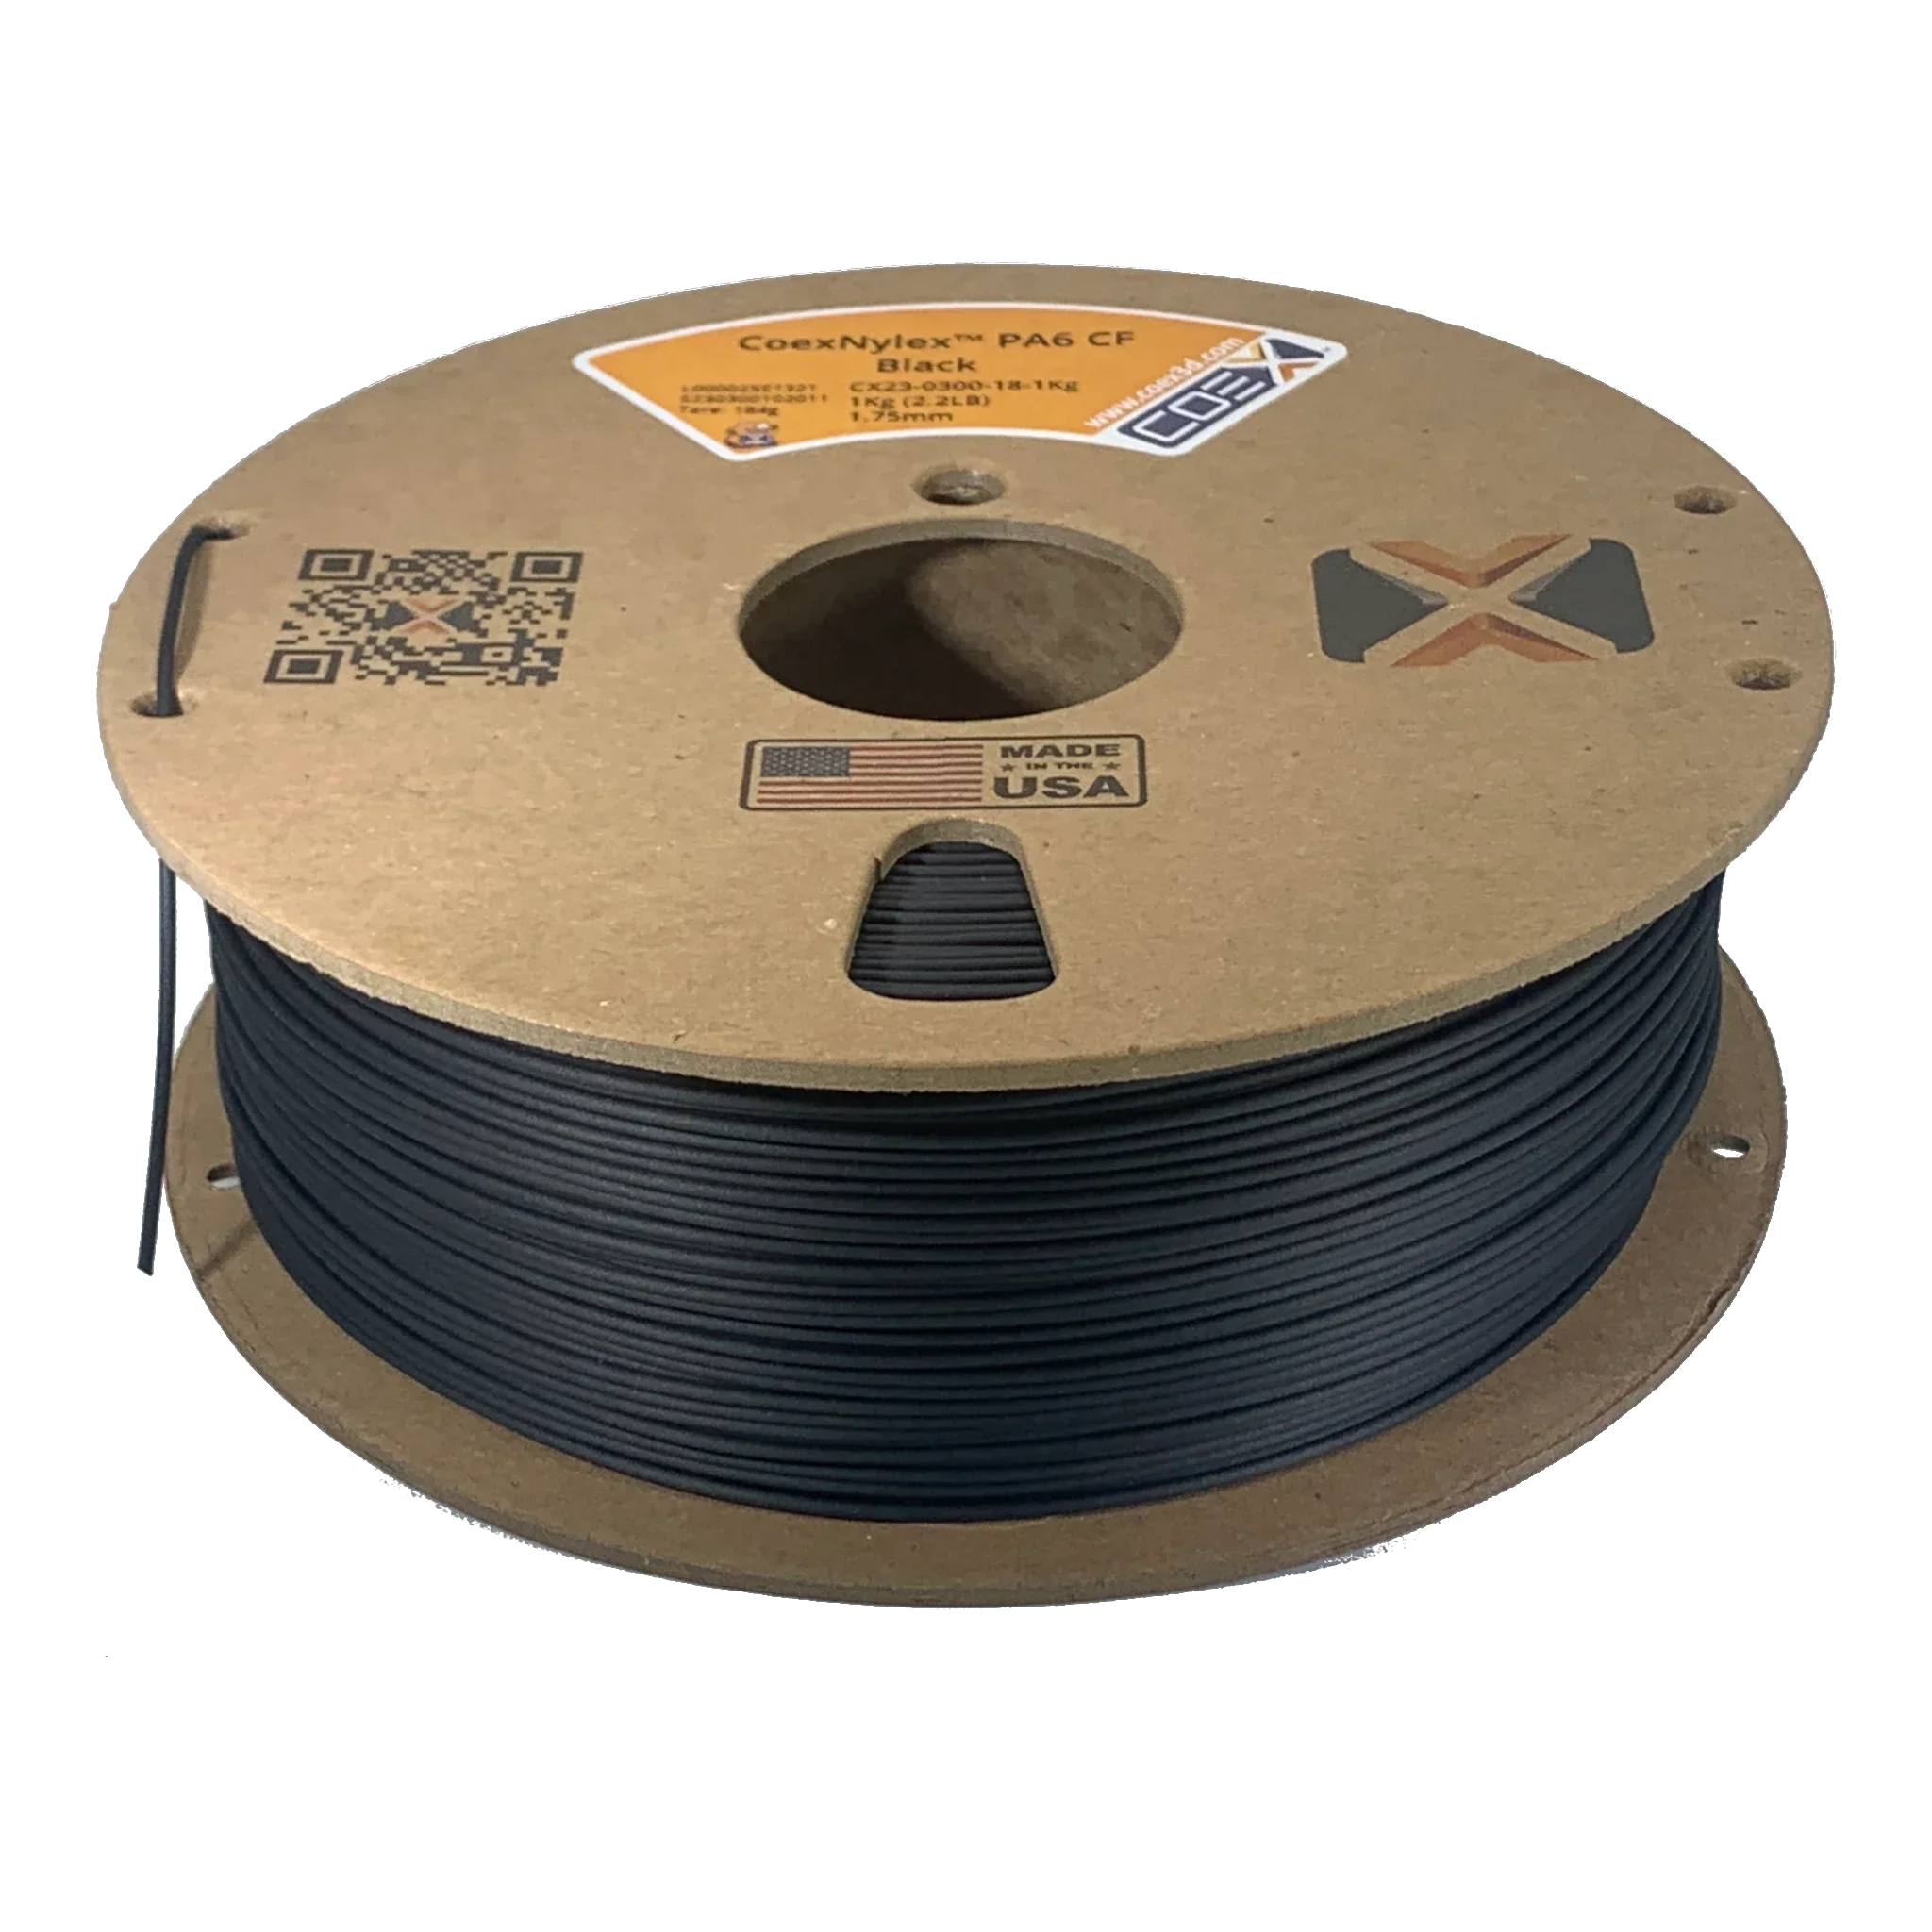
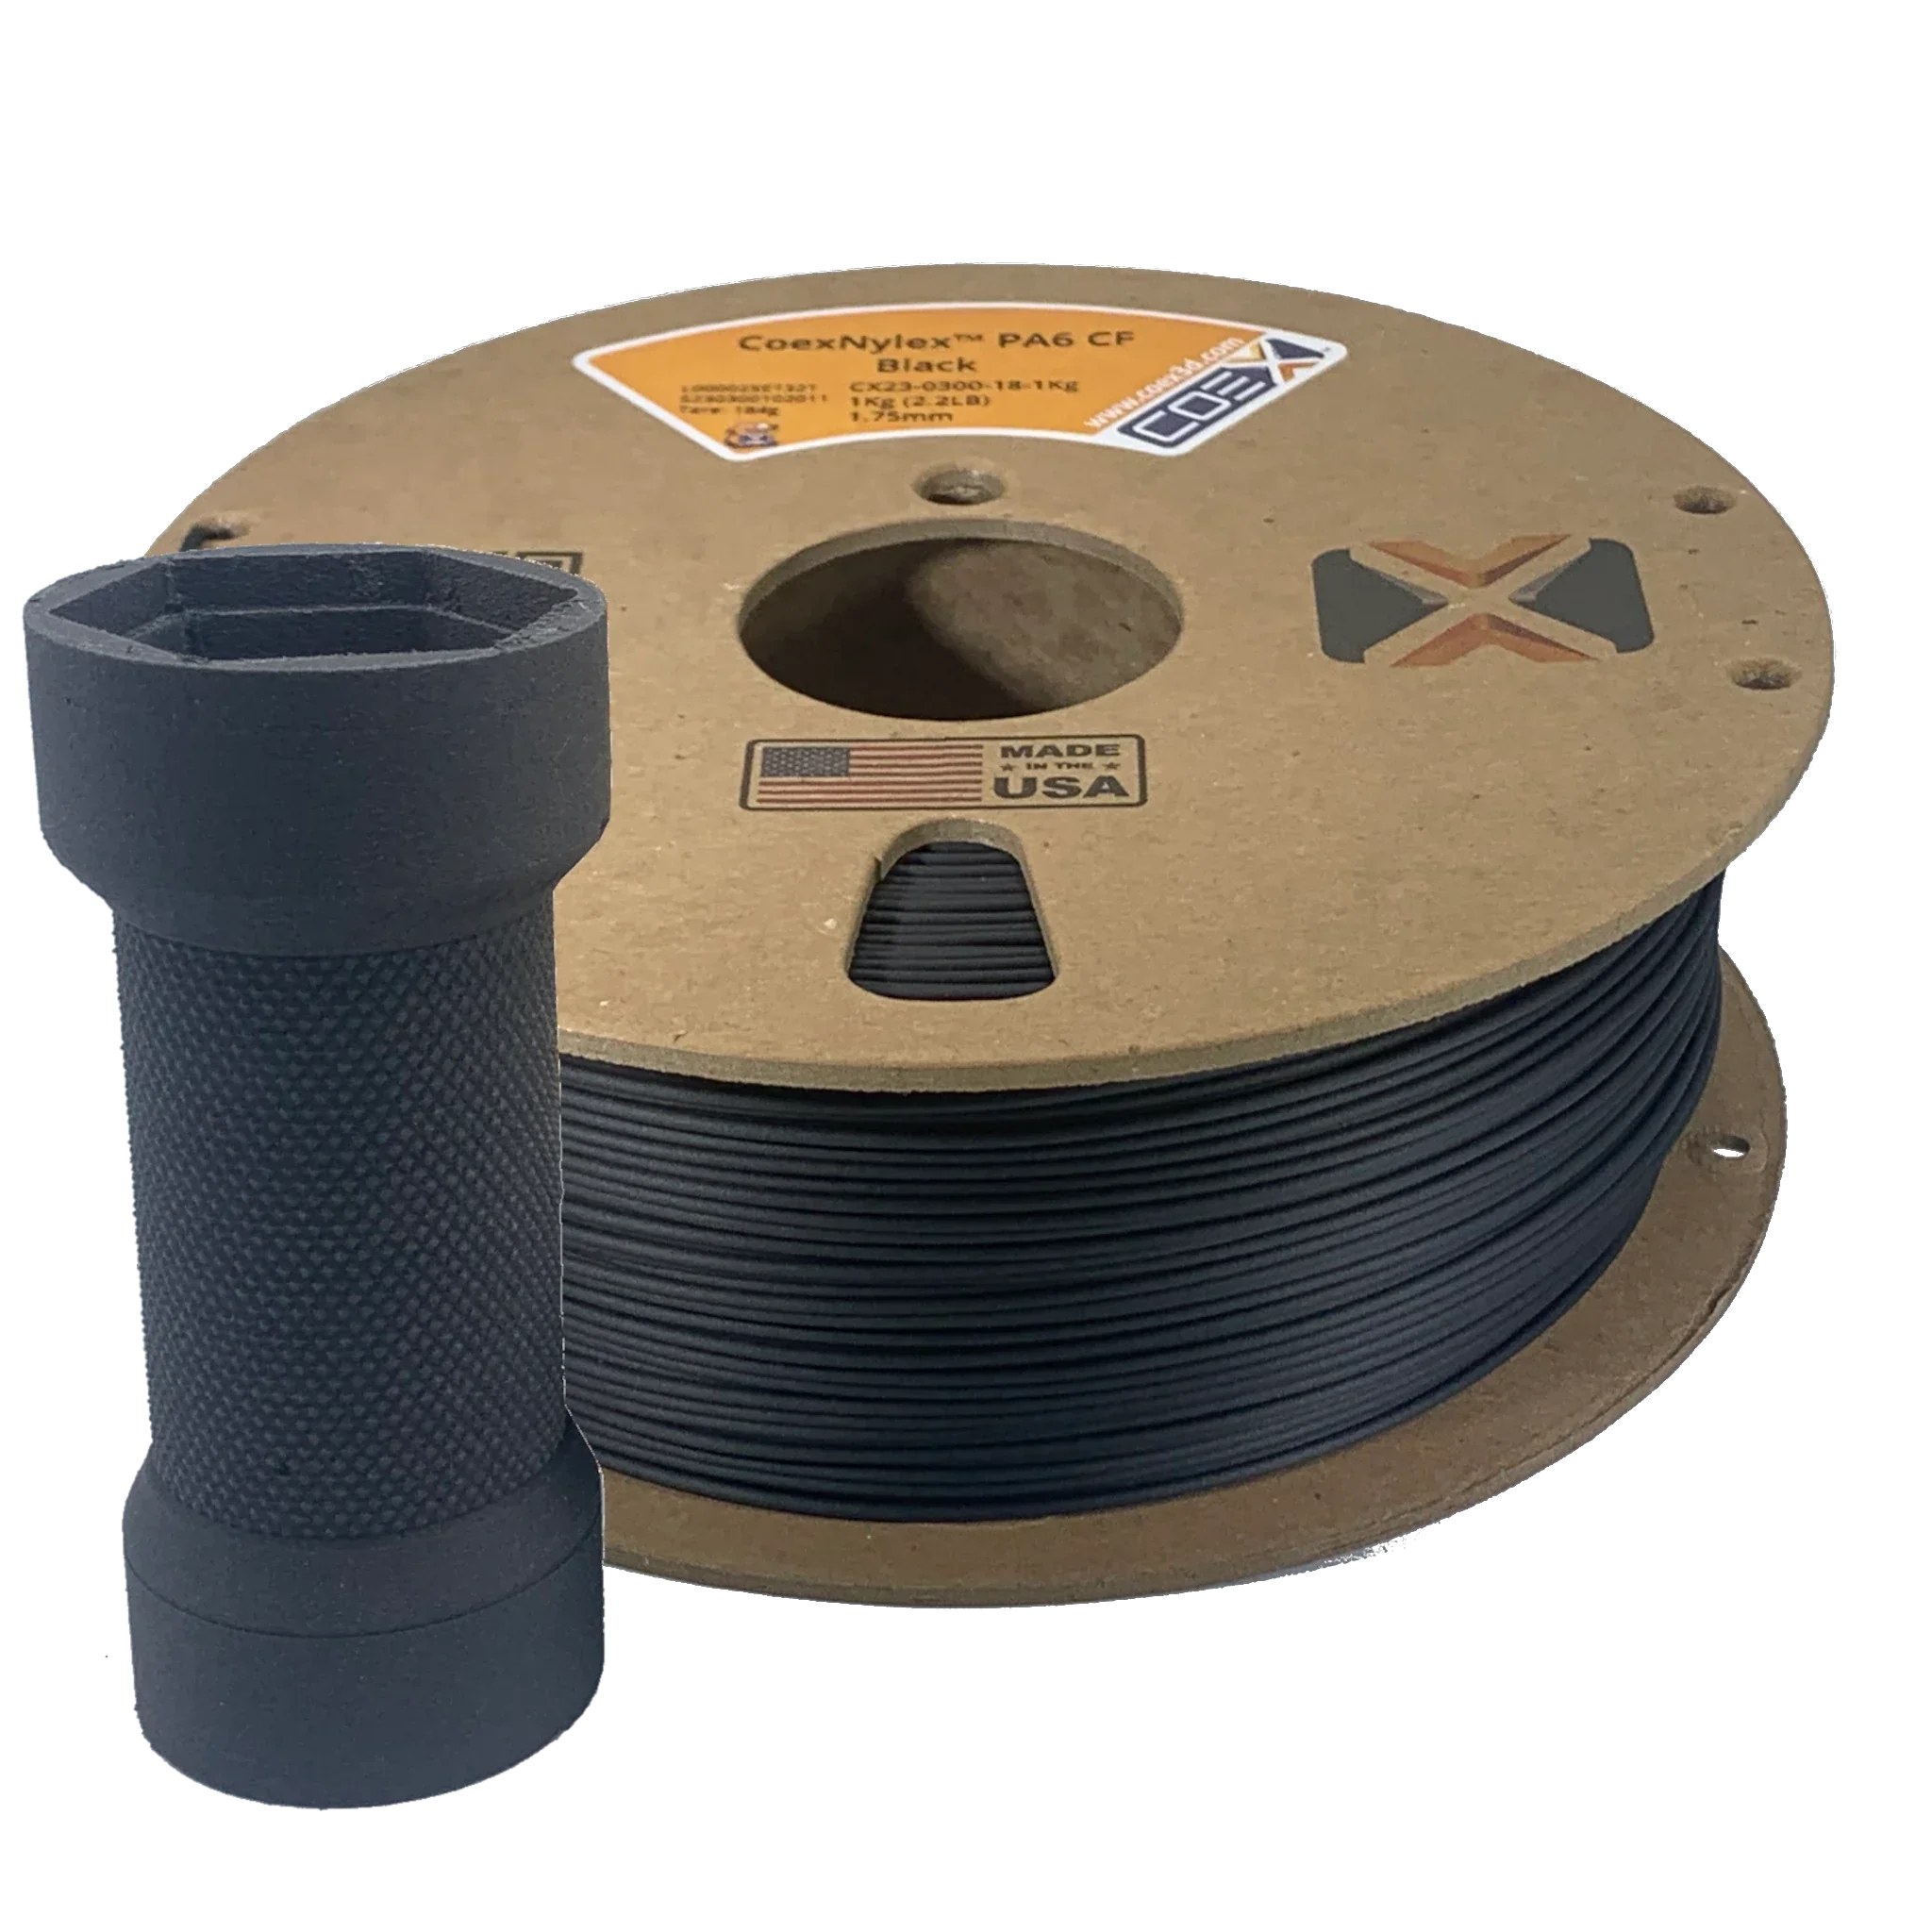
Black CoexNylex™ PA6-CF

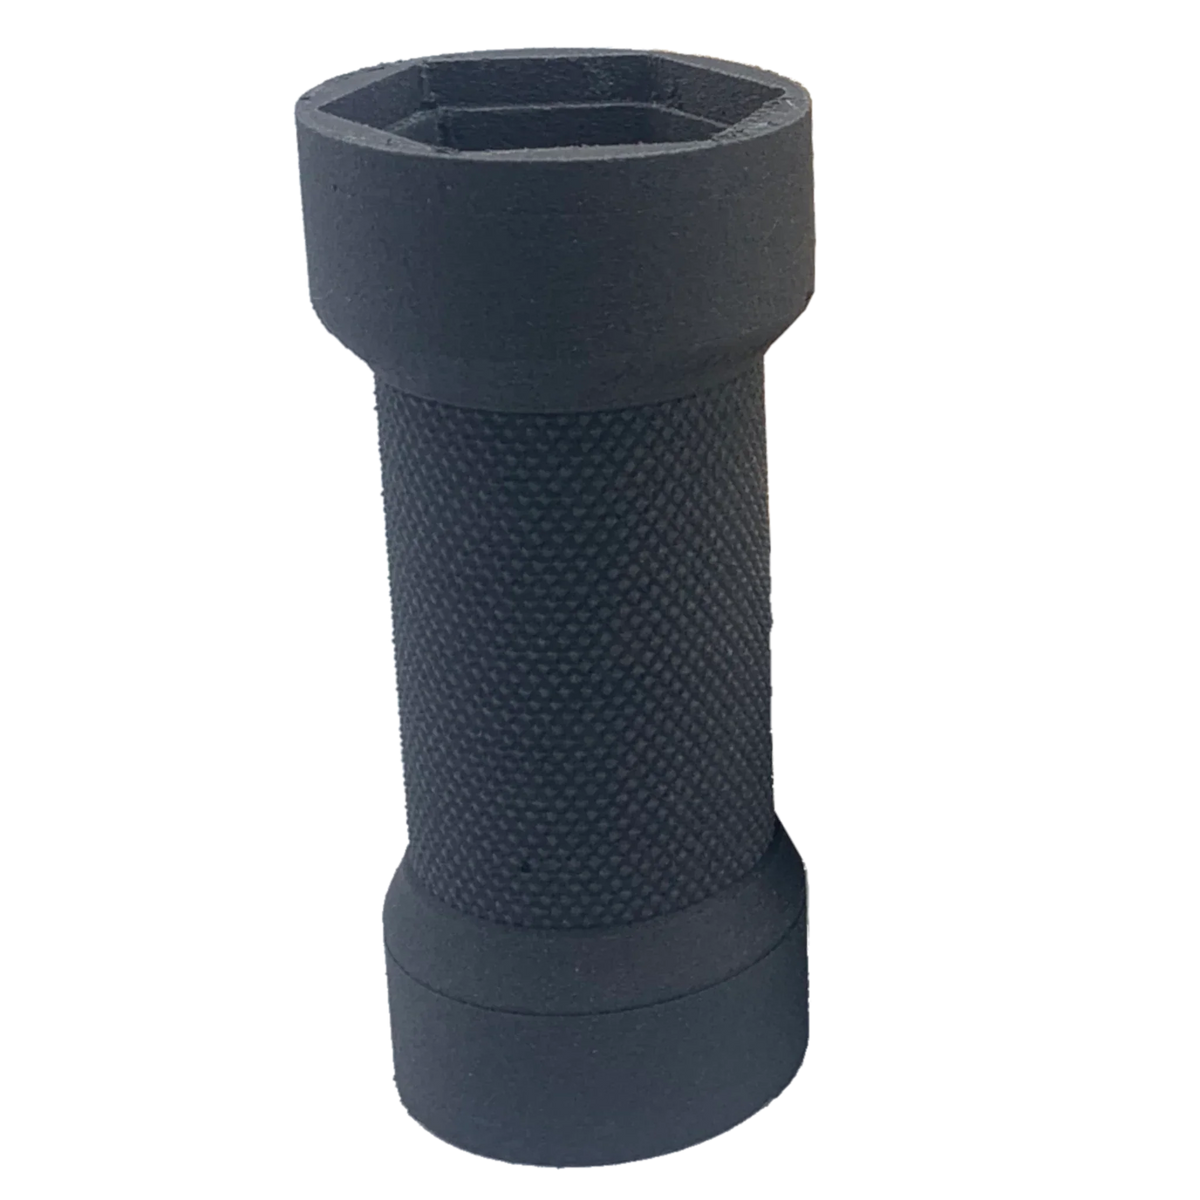
CoexNylex PA6-CF is PA6 nylon reinforced with 10% carbon fiber, and it's our top-selling nylon. Use it for parts that have to carry load, hold their dimensions and take heat: jigs, fixtures and manufacturing aids, robotics frames and mechanical components, automotive and aerospace prototypes, and load-bearing end-use parts. Want nylon without the fiber? See the full CoexNylex range.

Key properties

  • High strength-to-weight ratio and tensile strength
  • Dimensional stability and heat resistance for demanding engineering parts
  • Consistent extrusion and strong layer adhesion despite the fiber content
  • Matte black finish

Printing notes

  • Use a hardened steel or other wear-resistant nozzle. Carbon fiber wears brass.
  • Ships pre-dried, ready to print when you open it.
  • Nylon absorbs moisture. Reseal the spool with desiccant between prints, and dry an opened spool at 80°C for 8–12 hours before critical prints.
  • Need help dialing it in? Our engineering team can advise on settings.

Specs

  • Material: CoexNylex PA6 nylon with 10% carbon fiber
  • Diameter: 1.75mm, ±0.03mm
  • 1.75mm spools: 500g · 1kg
  • Vacuum-sealed with desiccant
  • Backed by our 100% satisfaction guarantee
  • Made in Green Bay, Wisconsin, USA
  • Slicer profile: the COEX NYLEX PA6-CF profile for 1.75mm filament is built into OrcaSlicer 2.3.2 and later. In Filament Selection, choose vendor COEX 3D, then COEX NYLEX PA6-CF.

Print settings · Slicer profiles · Technical data sheet · Safety data sheet

CoexNylex PA6-CF print settings

Print CoexNylex PA6-CF with a 265–290°C nozzle, an 80–100°C bed and an enclosure, with the fan at 40–80% (off for the first layer), and dry it at 80°C for 8–12 hours. It is abrasive, so use a hardened steel, ruby-tipped or other wear-resistant nozzle.

These are COEX 3D's recommended starting settings, made to match the COEX 3D filament settings tables for every filament we make in Green Bay, Wisconsin. Treat each value as a starting point and adjust it for your printer.

1. Material notes

  • Keep filament dry: store it sealed, and dry it again only after the spool has been exposed to air
  • Dry an opened spool at 80°C for 8–12 hours
  • An enclosure is required
  • PA6-CF is abrasive: use a hardened steel, ruby-tipped or other wear-resistant nozzle
  • Use a Z-offset slightly higher than for PLA (+0.05mm)
  • Enable "Avoid crossing perimeters" to reduce stringing
  • Consider using the "Wipe while retract" option
  • Enable "Slow down for small perimeters"
  • Print outer walls slower for better quality
  • Use a minimum layer time of 30 seconds for small parts
  • Consider using "Extra Prime Amount" after retraction

2. Temperature settings

Nozzle temperature: 265–290°C

Bed temperature: 80–100°C

  • Wash the bed often for good adhesion: use dish soap and rinse thoroughly to remove oils
  • Bed adhesion: use WELD3D or a PVA-based glue stick (e.g., Elmer's)
  • Use a brim for tall or large prints
  • Keep the ambient temperature stable

3. Basic parameters

CoexNylex PA6-CF basic parameters by nozzle size
Nozzle Layer height Line width Max volumetric speed Nozzle temperature
0.4mm 0.2mm 0.42mm 14.0 mm³/s 265°C
0.6mm 0.3mm 0.62mm 31.5 mm³/s 265°C
0.8mm 0.4mm 0.82mm 56.0 mm³/s 265°C
1.0mm 0.5mm 1.02mm 87.5 mm³/s 265°C

4. Speed settings

0.4mm nozzle (max volumetric speed 14.0 mm³/s)

CoexNylex PA6-CF speeds for a 0.4mm nozzle
Line type Percentage Speed
External perimeter 50% 83.33 mm/s
Internal perimeters 75% 125.00 mm/s
Infill 100% 166.67 mm/s
Top/bottom 60% 100.00 mm/s
First layer 30% 50.00 mm/s

0.6mm nozzle (max volumetric speed 31.5 mm³/s)

CoexNylex PA6-CF speeds for a 0.6mm nozzle
Line type Percentage Speed
External perimeter 50% 84.68 mm/s
Internal perimeters 75% 127.02 mm/s
Infill 100% 169.35 mm/s
Top/bottom 60% 101.61 mm/s
First layer 30% 50.81 mm/s

0.8mm nozzle (max volumetric speed 56.0 mm³/s)

CoexNylex PA6-CF speeds for a 0.8mm nozzle
Line type Percentage Speed
External perimeter 50% 85.37 mm/s
Internal perimeters 75% 128.05 mm/s
Infill 100% 170.73 mm/s
Top/bottom 60% 102.44 mm/s
First layer 30% 51.22 mm/s

1.0mm nozzle (max volumetric speed 87.5 mm³/s)

CoexNylex PA6-CF speeds for a 1.0mm nozzle
Line type Percentage Speed
External perimeter 50% 85.78 mm/s
Internal perimeters 75% 128.68 mm/s
Infill 100% 171.57 mm/s
Top/bottom 60% 102.94 mm/s
First layer 30% 51.47 mm/s

5. Retraction settings

Important: Set travel speed to the maximum your machine allows (200–500mm/s). Faster moves give the filament less time to ooze, which reduces stringing.

CoexNylex PA6-CF retraction by nozzle size
Nozzle Distance Speed Z-hop
0.4mm 1.0–1.5mm 40mm/s 0.2mm
0.6mm 1.0–1.5mm 40mm/s 0.2mm
0.8mm 1.0–1.5mm 40mm/s 0.2mm
1.0mm 1.0–1.5mm 40mm/s 0.2mm

6. Cooling settings

Cooling configuration:

  • First layer: 0% (fan off)
  • General printing: 40% base fan speed
  • Bridges and overhangs: 80% fan speed
  • Layers under 15 seconds: 40% fan speed

7. Troubleshooting

CoexNylex PA6-CF troubleshooting
Problem Solution
Irregular extrusion
  1. Dry the filament
  2. Check the extruder
  3. Reduce speed
Poor adhesion
  1. Dry the filament
  2. Use an adhesive
  3. Adjust the first layer
Stringing
  1. Dry the filament
  2. Adjust retraction
  3. Increase travel speed
  4. Check temperature

Please note: These printing parameters are initial recommendations based on our experience. They may need adjustment for your specific 3D printer, environmental conditions and the geometry of the part you are printing. Use them as a starting point and fine-tune them for your needs.
Coex 3D Filament Slicer Profiles

CX23 CoexNylex PA6-CF Technical Data Sheet

Technical Data Sheet: CX23 COEX-NYLEX CARBON FILLED SERIES 3D PRINTING FILAMENT

TDS Rev 1.0

BASE RESIN: Insight Polymers NBFC02

Physical Properties

PropertyStandardUnitTypical Value
Specific Gravity - DensityISO 1183g/cm³1.18
Melting Temperature, 10°C/minISO 11357-1/-3°C195

Mechanical Properties

PropertyStandardUnitTypical Value
Tensile StrengthASTM D638MPa76
Tensile ModulusASTM D638MPa3034
Yield % StrainASTM D638%4
Impact Strength (un-notched)ASTM D4812kJ/m²No Break

Thermal Properties

PropertyStandardUnitTypical Value
Drying Temperature @ 8 hours-°C80

SPECIFICATIONS

Filament Size:1.75mm(in)2.85mm(in)
MIN Diameter:1.72mm0.0677 in2.79mm0.1098 in
MAX Diameter:1.78mm0.0701 in2.91mm0.1146 in
Tolerance+/- .03mm+/- 0.0012 in+/- .06mm+/- 0.0024 in

ADVANTAGES

  • Heat Resistant, Chemical Resistant, Strong, Durable
  • Lightweight and incredibly strong material to make durable, functional parts.

Printed Specimen Conditions

Printer:Open Source FDM/FFF
Nozzle:0.4mm
Layer Height:0.25mm
Infill:100%, +/-45°
Extrusion Temp:245 - 295°C
Bed Temp:80 - 110°C
Specimen Orientation:XY Flat and Vertical
Printing Speed60mm/sec..

Disclaimer: The technical data contained on this data sheet is furnished without charge or obligation and accepted at the recipient's sole risk. This data should not be used to establish specifications limits or used alone as the basis of design. The data provided is not intended to substitute any testing that may be required to determine fitness for any specific use.

Download TDS (PDF)

CX23 CoexNylex PA6-CF Safety Data Sheet

Material Safety Data Sheet: CX23 PA6CF SERIES 3D PRINTING FILAMENT

MSDS

BASE RESIN: COEXNYLEX PA6CF

Issue Date: 05-12-2025

1. Identification of the substance/preparation of the company

1.1 Trade name:COEXNYLEX PA6CF 3D printer filament
1.2 Use of the product:3D printer filament, thermoplastic.
1.3 Supplier:1228 Elizabeth St
Green Bay, WI 54302
Phone: (920) 757-1055

2. Hazards identification

2.1 Classification:The product is not considered hazardous by 2012 OSHA Hazard Communication Standard: 29 CFR 1910.1200
2.2 Special advice on hazards:No specific dangers known.

3. Composition / information on ingredients

Chemical nameCAS No.Weight %Proprietary
Unspecified Nylon*70-95*
Carbon Fiber7440-44-05-30

The product contains no substances which at their given concentration are considered to be hazardous to health.

4. First-aid measures

4.1 On skin contact:In case of contact with molten polymer immediately cool the skin with cold water. Medical aid may be required to remove adhering material and for treatment of burns. The material is not likely to be hazardous by skin contact, but cleaning the skin after use is advisable.
4.2 After inhalation:Remove from exposure and move to fresh air immediately. If not breathing, give artificial respiration. If breathing is difficult, give oxygen. Get medical aid.
4.3 On ingestion:Drink plenty of water. Do not induce vomiting without medical advice. Call a physician immediately.
4.4 On eyes contact:In case of contact, immediately flush eyes with copious amounts of water for at least (15) minutes.

5. Fire-fighting measures

5.1 Suitable fire extinguishing media:Water spray, foam, dry powder.
5.2 Special exposure hazards:Hazards during fire-fighting: Ammonium hydroxide, carbon monoxide, carbon dioxide, hydrocarbons, nitriles, and hydrogen cyanide can be emitted at > 320 °C.
5.3 Special protective equipment:Self-contained breathing apparatus
5.4 Remark:In case of fire and/or explosion do not breathe fumes.

6. Accidental release measures

6.1 Personal precautions:Spilled material may cause a slipping Hazard.
6.2 Methods for cleaning up:Vacuum or sweep up material and place into a suitable disposal container.

7. Handling and storage

7.1 Handling:Avoid contact with molten polymer. Avoid inhalation of dusts/mists/vapors.
7.2 Storage:Protect against moisture. Store cool and keep packaging closed when not in use. Avoid sources of ignition.

8. Exposure controls/ personal protection

8.1 Technical safety measures:This product, as supplied, does not contain any hazardous materials with occupational exposure limits established by the region-specific regulatory bodies.
8.2 Personal safety equipment:Use adequate safety equipment, e.g. protective clothing, eye protection glasses, heat protection gloves. Additives in this product do not present a respiration hazard unless the product is ground to a powder of respirable size and the dust is inhaled. All dusts are potentially injurious to the respiratory tract if respirable particles are generated and inhaled. A respiratory protection program that meets country requirements must be followed whenever workplace conditions warrant respirator use. Consult the respirator manufacturer to determine the appropriate type of equipment for a given application. Observe respirator use limitations specified by the manufacturer. Consult the OSHA respiratory protection information located at 29CFR 1910.134. Use a positive pressure air supplied respirator if exposure levels are not known or there are any other circumstances where air purifying respirators may not provide adequate protection.
8.3 Work hygiene:No eating or drinking during working. Avoid contact of hot material with the skin. Avoid breathing dust and vapors.

9. Physical and chemical properties

9.1 Form:Spool
9.2 Color:Various
9.3 Odor:None
9.4 Melting Temperature:195C
9.5 Oxidizing properties:No test data
9.6 Explosions limits:No test data
9.7 Density:1.18 g/cm³
9.8 Solubility in water:Not soluble

10. Stability and reactivity

10.1 Stability:The product is stable at recommended storage conditions.
10.2 Conditions to be avoided:Temperature: > 320 degrees Celsius
10.3 Substances to be avoided:No special recommendations.
10.4 Hazardous decomposition products:Hazardous decomposition products: Ammonium hydroxide, carbon monoxide, carbon dioxide, hydrogen cyanide, nitriles. Thermal decomposition: > 320 °C

11. Toxicological information

11.1 Local irritation:None
11.2 Other remarks:Assessment of irritating effects: Irritation is possible when the product comes in contact with the skin, respiratory tract or the eyes. Thermal decomposition products of the substance can irritate the eyes, skin, and respiratory tract.

12. Ecological information

12.1 Ecological info:The product has not been tested. There is a high probability that the product is not acutely harmful to aquatic organisms.
12.2 Biological degradation:Experience shows this product to be inert and non-degradable. The product is virtually insoluble in water and can thus be separated from water mechanically in suitable effluent treatment plants.
12.3 Bioaccumulation:The product will not be readily bioavailable due to its consistency and insolubility in water.

13. Disposal considerations

13.1 Product:In accordance with local and national regulations. Should not be released into the environment. Do not contaminate ponds, waterways or ditches with chemical or used container.
13.2 Uncleaned packaging:Packaging material has to be emptied completely and disposed in accordance with the regulations. Packaging can be recycled if not contaminated.

14. Transport information

14.1 Transport regulations:Not classified as hazardous under transport regulations DOT, ICAO/IATA, IMDG/GGVSee, ICAO/IATA

15. Regulatory information

15.1 U.S. Toxic Substances Control Act (TSCA):Complies
15.2 SARA 313:This product does not contain any chemicals which are subject to the reporting requirements of the ACT and Title 40 of the Code of Federal Regulations, Part 372.

16. Other information

16.1 NFPA Hazard codes: Health: 1, Flammability: 1, Reactivity: 0

16.2 HMIS III Rating: Health: 1, Flammability: 1, Physical hazard: 0

This data is based on the current state of our information and experience. This safety data sheet describes our product in terms of safety requirements. Preceding data is not applicable as a warranty of product properties. It is the responsibility of the recipient to observe the existing legal regulations for the use of this product.

Disclaimer: The safety data contained on this data sheet is furnished without charge or obligation and accepted at the recipient's sole risk. This data describes our product in terms of safety requirements. The data provided is not applicable as a warranty of product properties. It is the responsibility of the recipient to observe the existing legal regulations for the use of this product.

Download SDS (PDF)

Black CoexNylex™ PA6-CF

SKU: CX23-0300-18-1KG
3 reviews

Diameter: 1.75mm
Weight: 1kg
Price:
Sale price$85.00
Stock:
Stock: 0, We will be making more soon

You may also like

Recently viewed